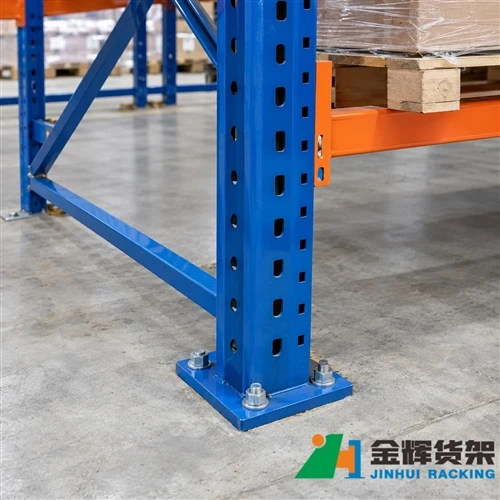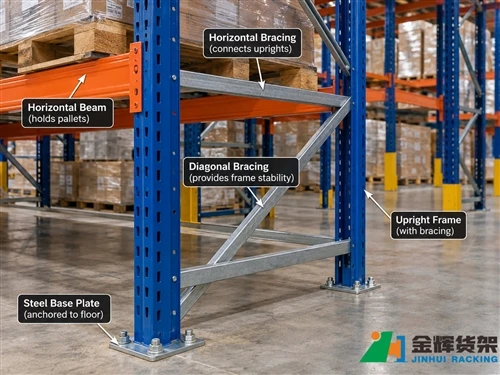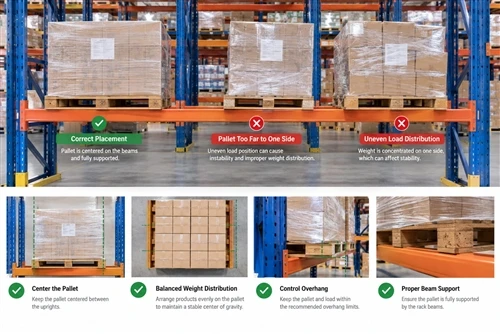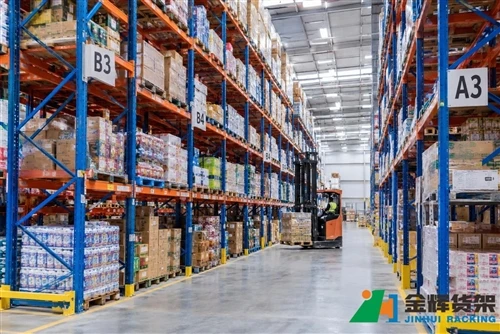
A drive-in rack is a type of storage system used in industrial applications to store and organize pallets of goods. It consists of a series of vertical upright frames connected by horizontal beams, which support the pallets at different levels. Unlike traditional pallet racks, drive-in racks are designed to allow forklifts to drive into the rack structure, making it easier to access and retrieve pallets.
Drive-in racks are available in different configurations and sizes to suit specific storage requirements. They can be single-deep or double-deep, depending on the space available and the type of goods being stored. Drive-in racks can also be adjustable, allowing the beams to be raised or lowered to accommodate pallets of different heights.
One of the key benefits of drive-in racks is their efficiency. By allowing forklifts to drive into the rack structure, they reduce the need for aisle space between racks, maximizing the use of floor space. This makes drive-in racks an ideal solution for storing large quantities of pallets in a limited space.
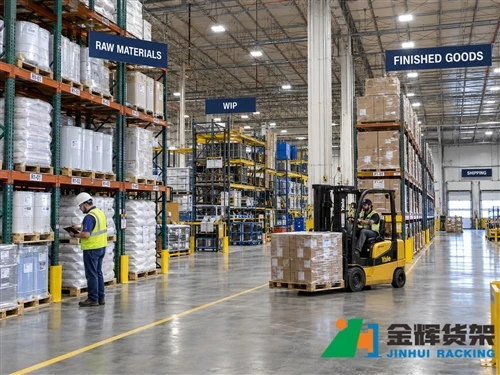
Drive-in racks are also highly versatile, able to store a wide range of goods, including raw materials, finished products, and packaging materials. They can be easily reconfigured to accommodate changes in storage needs or product mix, making them a flexible solution for industrial applications.
In addition to their efficiency and versatility, drive-in racks are also cost-effective. They are relatively inexpensive to install and maintain, and can be used for many years with proper care and maintenance. Drive-in racks can also be customized to fit specific storage needs, reducing the need for costly modifications or additional storage equipment.
Overall, drive-in racks are an efficient and versatile storage solution for industrial applications. With their cost-effectiveness, adaptability, and maximized use of floor space, they offer a reliable and effective way to store and organize pallets of goods in warehouses, distribution centers, and manufacturing facilities.